


1/8″ SHAFT
Detail + access
Small rotary tools, flex-shaft handpieces and micromotors bring control to details and tight spaces.
Connection check
Use a matching 1/8″ collet or approved chuck. Check the handpiece and burr speed ratings.


KUTZALL RESOURCES
Start with the tool in your hands.
Match your power tool to the right Kutzall accessory. Start with the connection, then check speed, mounting hardware and clearance.
Find your setupAlready own a grinder? Check its exact model and manual before choosing an accessory.
THREE STARTING POINTS
Choose by the connection: burr shafts fit the collet; Shaping Wheels seat on the mounting flange. Hand drills and drill presses are not recommended for rotary burrs.
Small rotary tools, flex-shaft handpieces and micromotors bring control to details and tight spaces.
Use a matching 1/8″ collet or approved chuck. Check the handpiece and burr speed ratings.
Die grinders and compatible flex-shaft handpieces give larger burrs the power for more substantial shaping.
Use a matching 1/4″ collet. A smaller burr needs the correct collet or approved reducer.
Angle grinders cover broad surfaces, blend curves and bring larger forms into shape.
Match wheel diameter, guard, flange and nut. A 5/8″ shaft does not mean a 5/8″ wheel bore.
LOOK BEYOND THE SHAFT
The guard must suit the wheel diameter and let the wheel rotate freely. Its back shape matters.
Many Type 27 guards provide the clearance a Shaping Wheel needs. Confirm your exact grinder and guard combination.
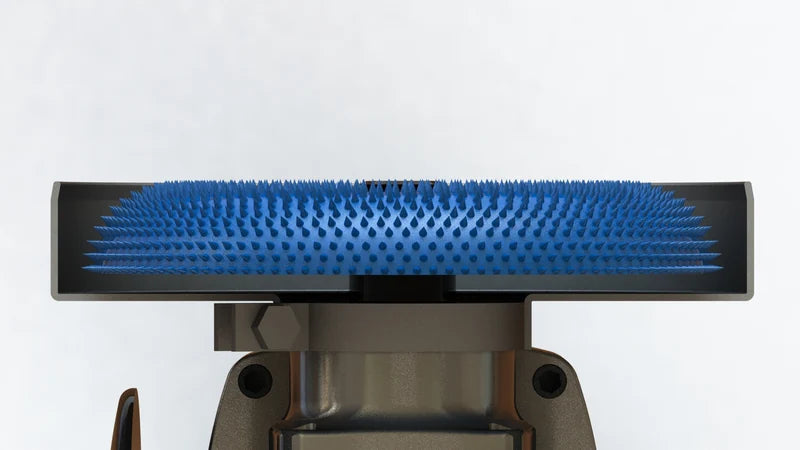
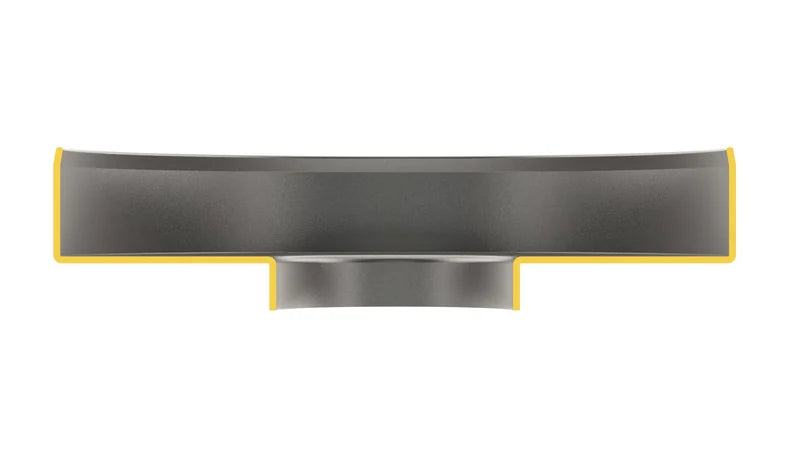
Guards made only for depressed-center wheels can rub against a Kutzall wheel. A small chamfer alone is not necessarily a problem.
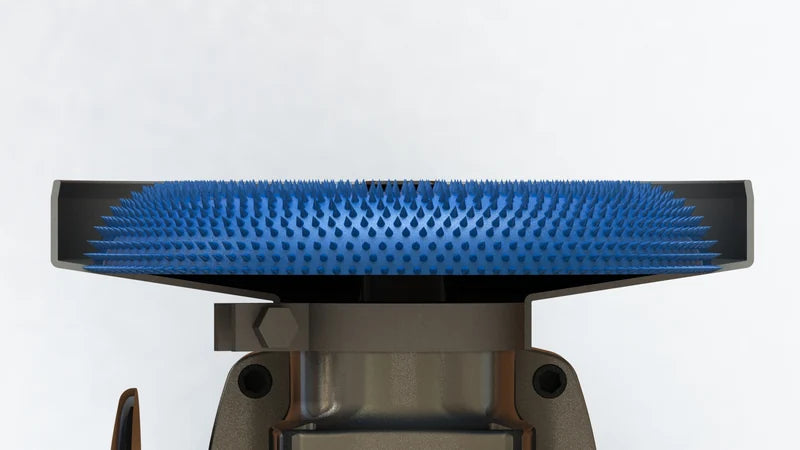
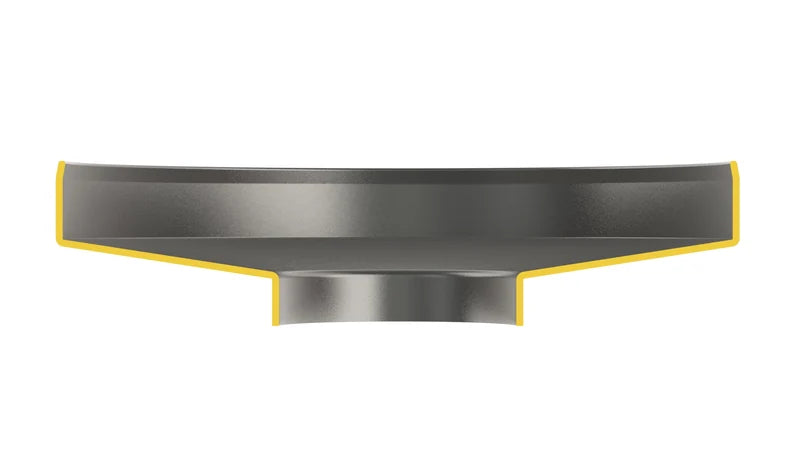
Illustrations compare back-profile clearance only. Guard type, wheel diameter and your grinder’s instructions must also match.
Type 1 cut-off guards are unsuitable. Keep the correct guard fitted; do not modify it to make a wheel fit.
The wheel’s 7/8″ bore seats on the flange shoulder, not directly on the grinder shaft.
Fast braking can loosen the mounting nut with heavier accessories. Confirm wheel and mounting-hardware compatibility with the grinder manufacturer.
FIND YOUR MODEL
Use these model references as a starting point. Confirm the exact collet, speed range and approved accessories with the manufacturer.
Specifications and availability can change. Manufacturer links open in a new tab.
K.1040 and K.1050 need the 1/8″ collet configuration. H.44T uses a key-tip flex shaft; H.44HT uses square drive. Listed die grinders need a suitable 1/8″ collet or approved reducer.
Use a 1/4″ collet. H.44T and H.44HT need the matching flex-shaft drive. K.1040 and K.1050 micromotor kits are listed under 1/8″ burrs.
Confirm wheel capacity, guard clearance, flange and nut, speed rating and braking compatibility.
CHOOSE HOW YOU WORK
Compare handling, speed and power source. Open a topic for the practical differences.

